Skip to content

We pick the process for the part, not the other way round.

FDM runs in our own studio, powder printing and resin at vetted workshops in Poland. When a run is cheaper another way, we prepare the documentation and place the order.

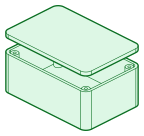
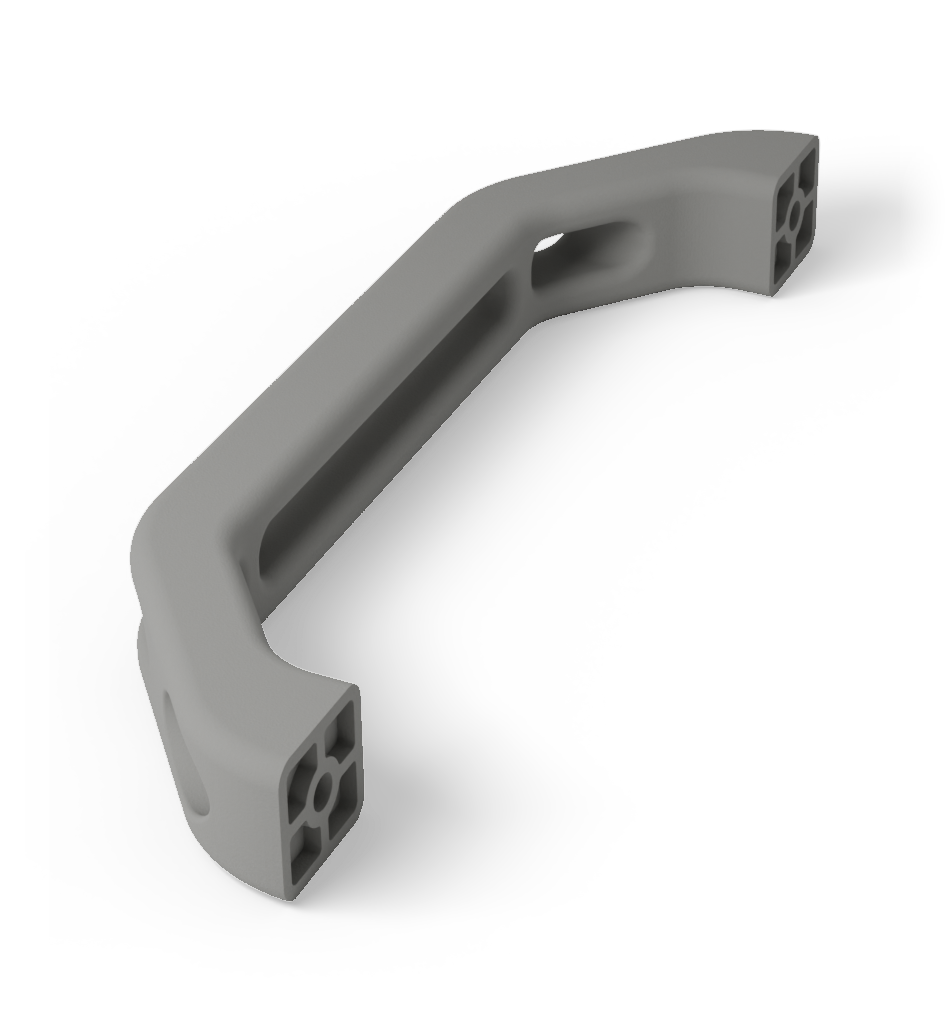
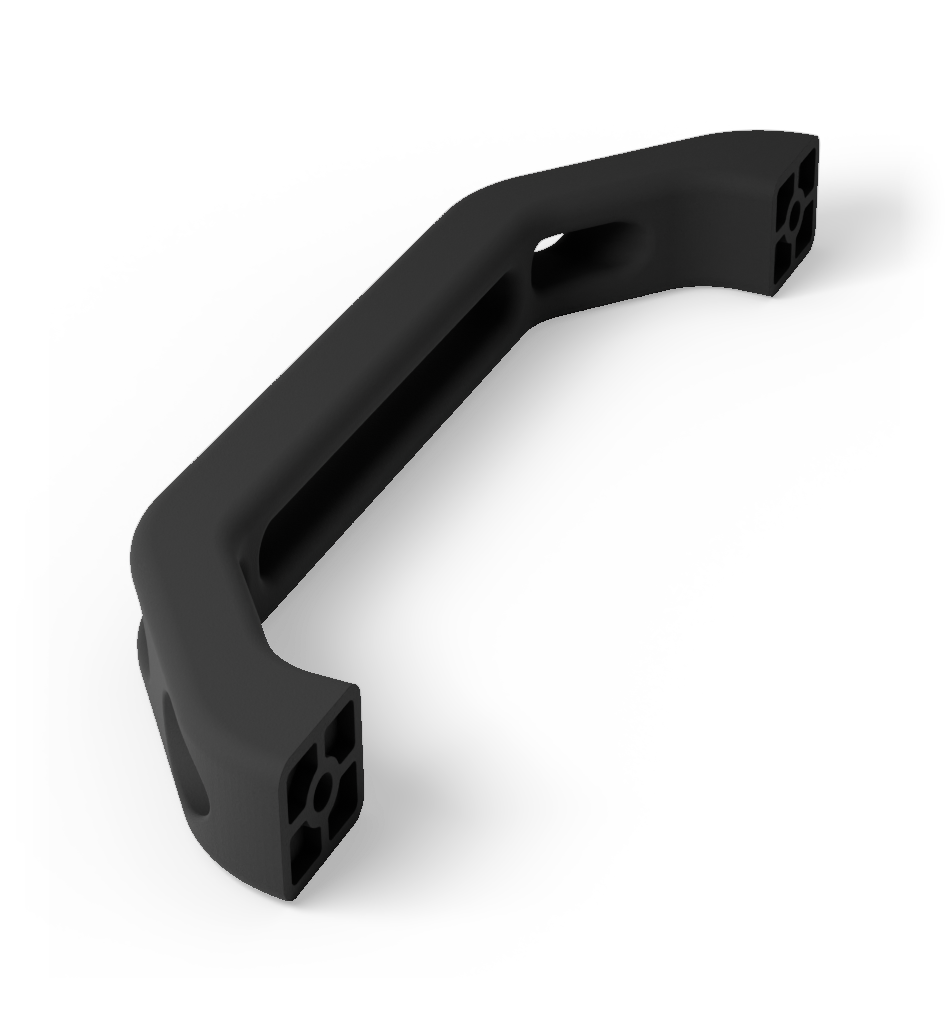
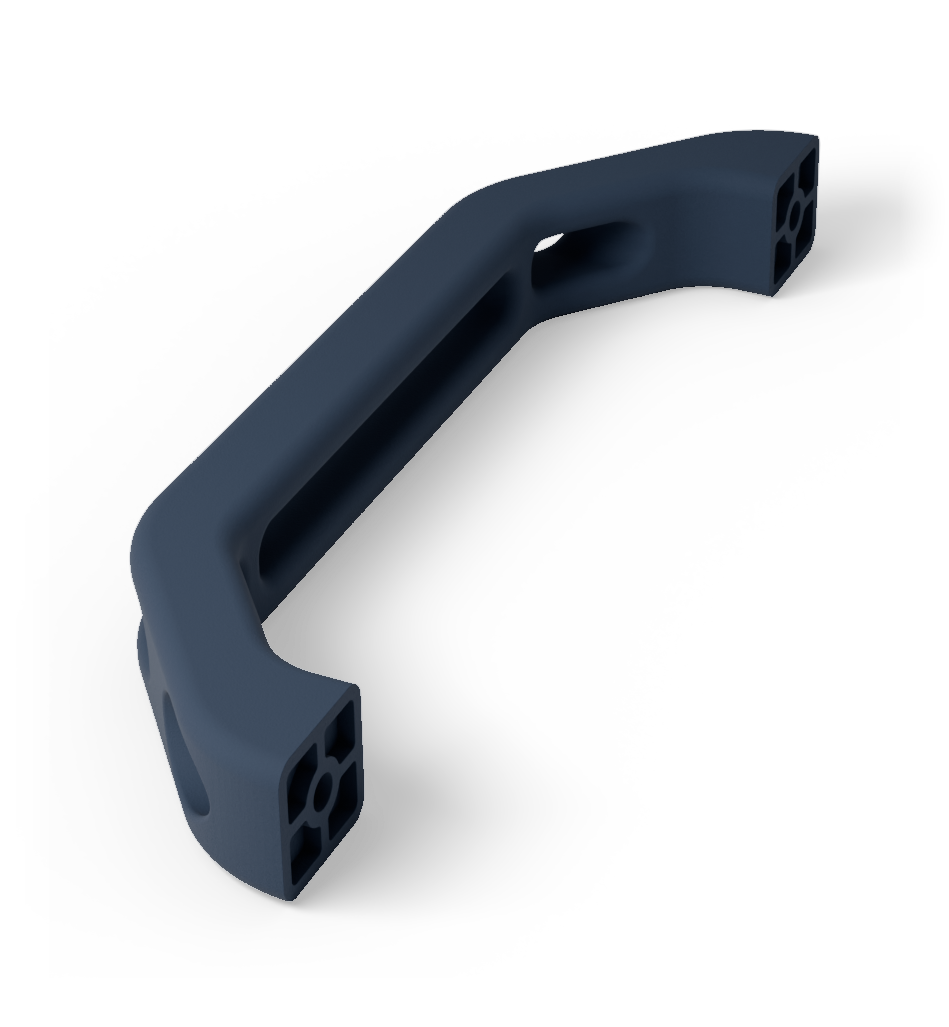
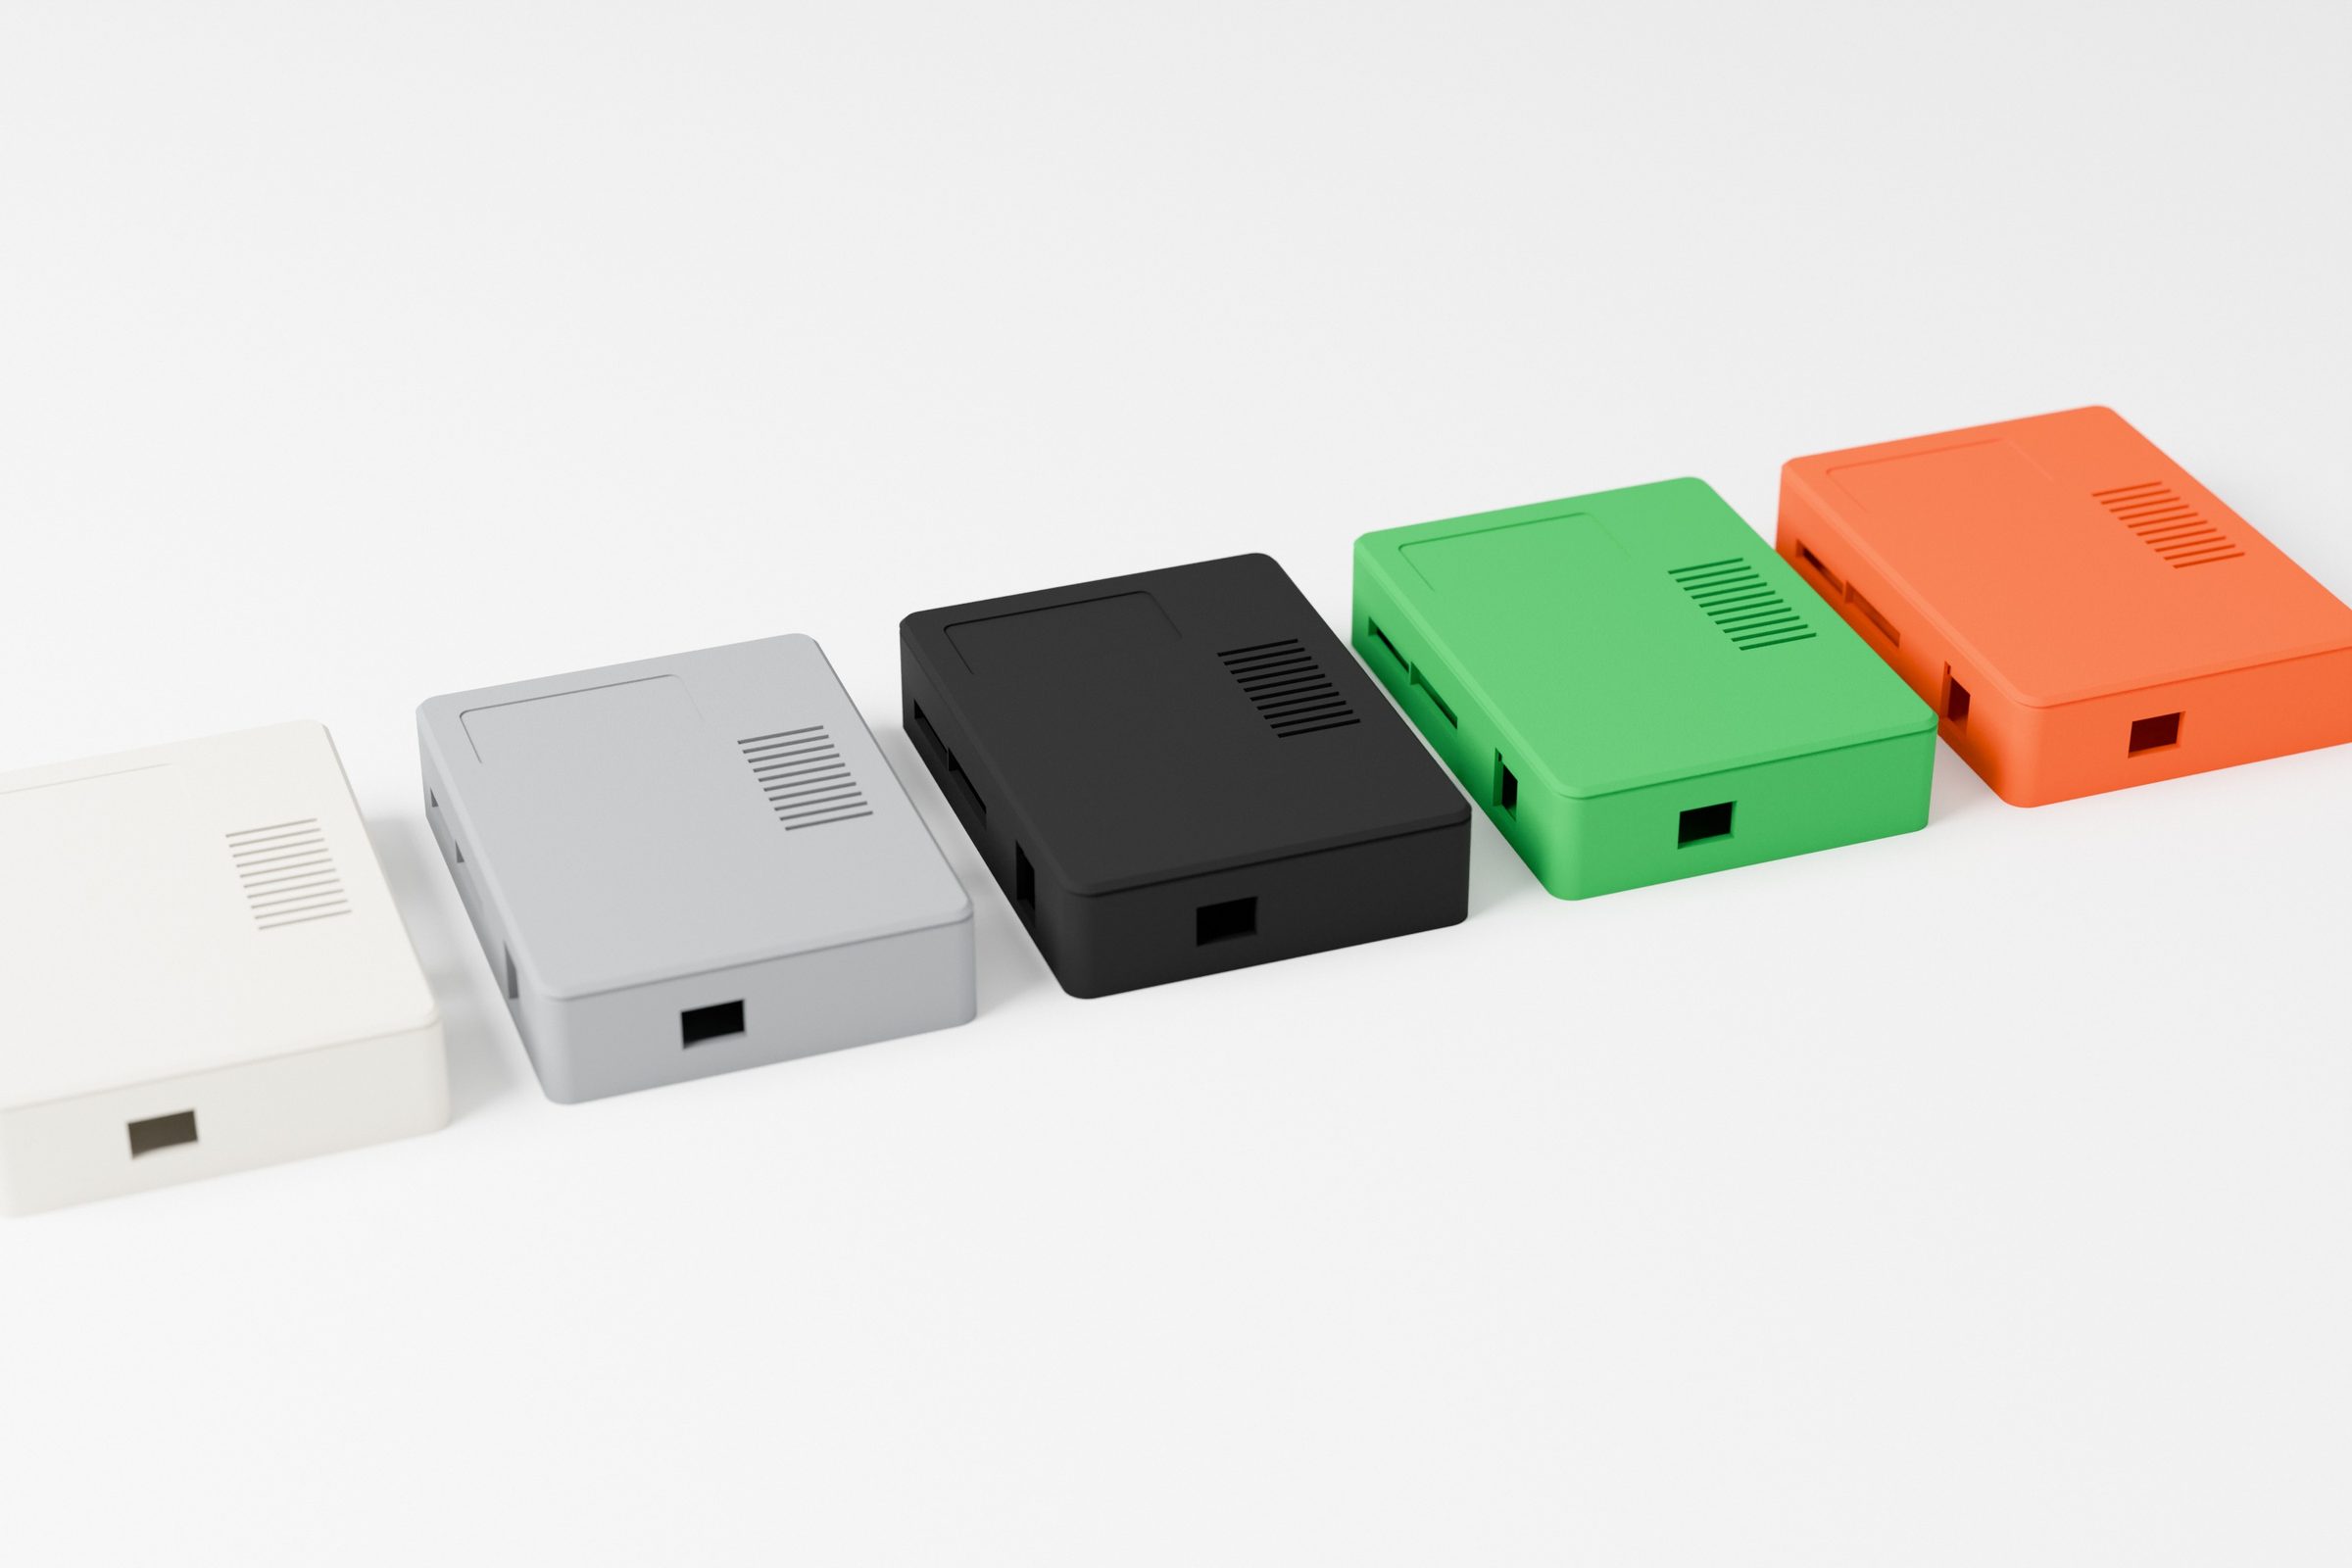
Visualisation: electronics enclosures in different colours and finishes

Five questions instead of material names.

You don't need to know PA12 or ASA. The answers point to the process.

  1. 1

    Load

    1. plain plasticholder · PETG
    2. nylonlever, snap fit · PA12
    3. metalshaft, frame

    A holder we print in plain plastic, a loaded lever in nylon, and a shaft in metal.

  2. 2

    Temperature

    1. up to 55 °Cplain plastic · PLA
    2. up to 95 °Cheat resistant · ASA
    3. up to approx. 175 °Cnylon · PA12
    4. highermetal

    Up to that temperature the plastic keeps its shape under load. Next to an engine or a furnace, metal wins.

  3. 3

    Environment

    1. sun and frostUV resistant · ASA
    2. oil and fuelnylon · PA12
    3. has to flexrubber-like · TPU

    Outdoors we print in a plastic that won't fade or turn brittle. Around oil, nylon does the job.

  4. 4

    Size

    1. up to 256 mmone piece in-house
    2. largersegments, panel, sheet metal

    Up to 256 mm we print in one piece. Larger parts we split into segments or make from panels and sheet metal.

  5. 5

    Quantity

    1. plastic printing1 to a few
    2. powder printingtens and hundreds
    3. injection mouldthousands

    For a few parts a mould doesn't pay. For thousands, printing doesn't.

When in doubt, we print a test version first.

Four printing processes.

Each one is best at something. The dots are a rough rating against the other three.

FDM

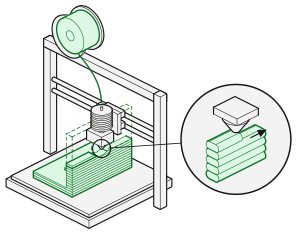
Plastic from a spool melts in the nozzle and is laid down path by path, in 0.1-0.3 mm layers. The cheapest route to a prototype, a holder or a jig.

in-house, Opole · 2-4 days
strength
detail
smoothness
low unit cost
Drawing: how FDM works
Layers show on curves
A lattice inside, not solid plastic

Best for

  • Sensor holder
    Sensor holder
  • Assembly jig
    Assembly jig
  • Guard
    Guard
  • Prototype housing
    Prototype housing

A part that proves itself can stay in FDM or move to MJF.

Strengths and limitations

Plastic from a spool is melted and laid down path by path, layer by layer. It is our in-studio tool: the shortest route from a model to a first part in your hand.

Strengths

  • Fastest start and easy iteration: change the model, print again
  • Wide choice of plastics and colours
  • Low cost per single part

Limitations

  • Visible layer lines on the surface
  • Parts are weaker along the layers, so print orientation matters
  • Overhangs need supports that leave marks

Materials: PLA, PETG, ABS, ASA, TPU.

Adapter reverse-engineered and printed in PETG-CF and PETG →
MJF

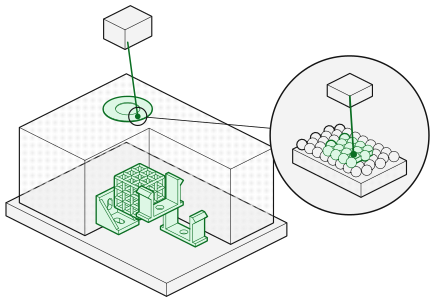
A print head applies a fusing agent to a layer of polyamide powder and a lamp fuses it. Strong parts without supports, good for runs.

at a partner · 3-5 days

strength
detail
smoothness
low unit cost
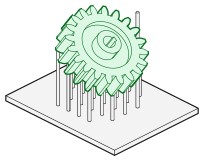
Drawing: how MJF works
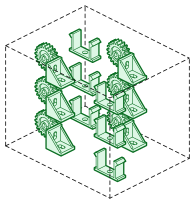
A whole chamber in one build
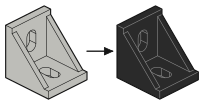
Grey off the machine, then dyed

Best for

  • Snap clip
    Snap clip
  • Hinged housing
    Hinged housing
  • Plastic gear
    Plastic gear
  • Profile connector
    Profile connector

Parts fill the whole chamber, so in a run each one comes out cheap. Off the machine they are grey; we dye them dark colours.

Strengths and limitations

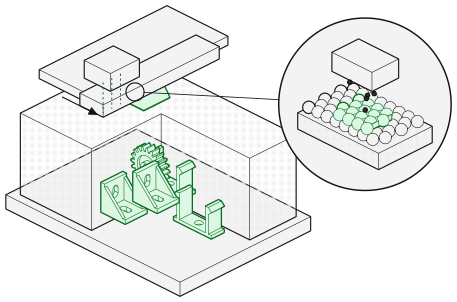
A print head applies a fusing agent to a thin layer of polyamide powder and heat fuses the marked areas. Parts grow without supports, surrounded by powder, so one build can hold many parts at once.

Strengths

  • Similar strength in every direction
  • Repeatable dimensions across a run
  • After vapour smoothing the surface comes close to a moulded part

Limitations

  • Natural colour is grey, so parts are dyed black or dark; light colours only from SLS
  • Walls from about 1 mm; small deep holes trap powder
  • Size limited by the machine's build chamber

Materials: PA12, PA11, powder TPU. Typical tolerance ±0.3 %, no tighter than ±0.3 mm.

Pontiac armrest: STEP model prepared for MJF / SLS →

SLS

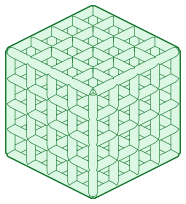
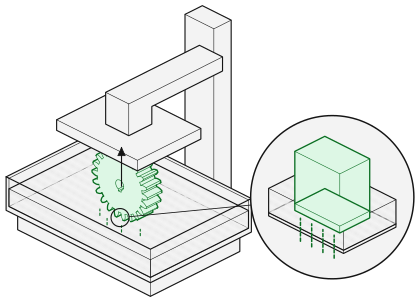
A laser sinters polyamide powder layer by layer. The powder holds the part up, so no supports are needed.

at a partner · 3-5 days

strength
detail
smoothness
low unit cost
Drawing: how SLS works
Lattice without supports
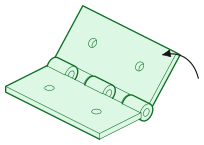
A hinge in one print

Best for

  • Vent grille
    Vent grille
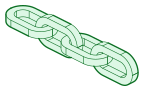
  • One-piece chain
    One-piece chain
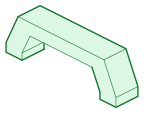
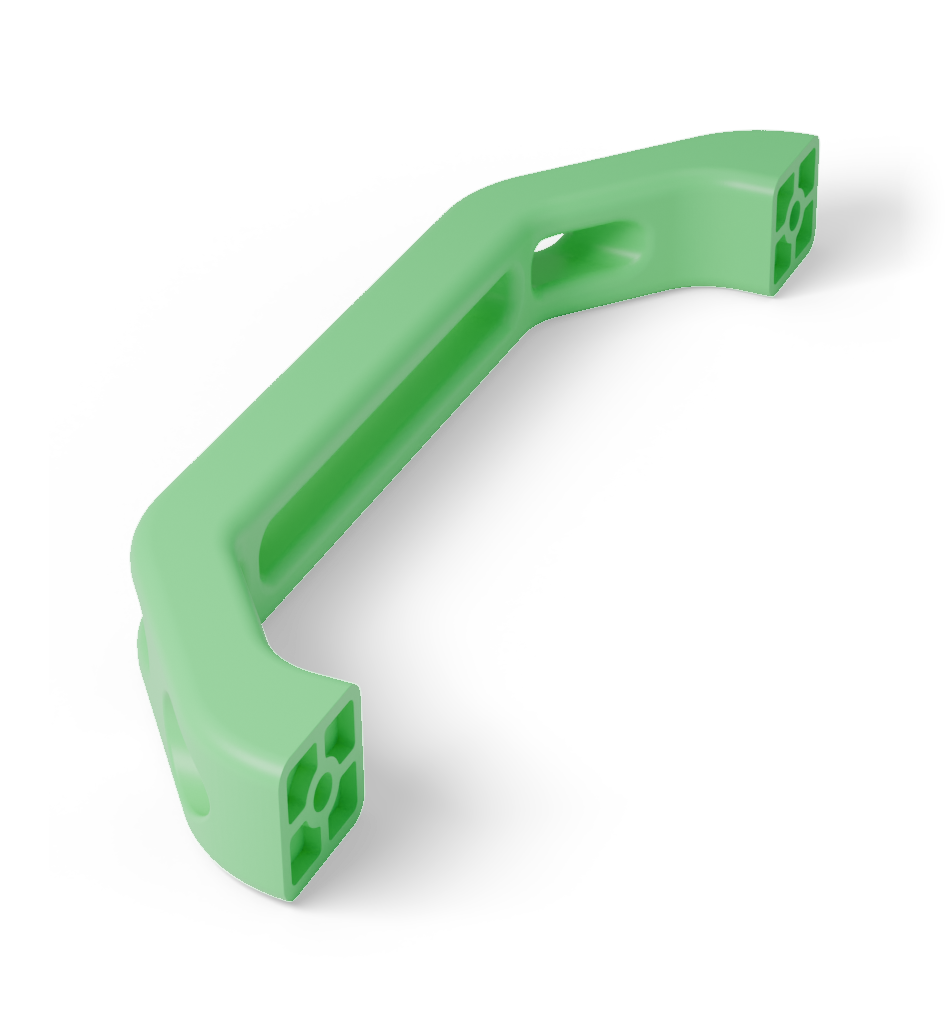
  • Handle
    Handle
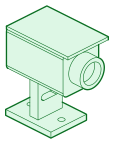
  • Camera housing
    Camera housing

White powder can be dyed light colours too. Moving parts are printed already assembled.

Strengths and limitations

A laser sinters polyamide powder layer by layer. As with MJF, parts need no supports, and the naturally white powder can also be dyed in light colours.

Strengths

  • Shape freedom without supports
  • White base: the widest choice of dye colours
  • Strong, resilient parts in PA12 and PA11

Limitations

  • The raw surface is matte and slightly grainy
  • Walls from about 1 mm
  • Size limited by the machine's build chamber

Materials: PA12, PA11, powder TPU. Typical tolerance ±0.3 %, no tighter than ±0.3 mm.

Pontiac armrest: STEP model prepared for MJF / SLS →

Resin

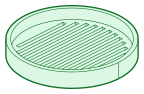
Light cures liquid resin layer by layer, 0.025-0.1 mm at a time. The finest detail and the smoothest surface of the four.

at a partner · lead time in the quote

strength
detail
smoothness
low unit cost
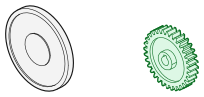
Drawing: how Resin works
Supports we cut off afterwards
Fine teeth next to a coin

Best for

  • Casting pattern
    Casting pattern
  • Small precise gear
    Small precise gear
  • Scale model
    Scale model
  • Clear cover
    Clear cover

Resin dislikes sunlight and heavy loads. We use it when detail, a pattern or looks matter.

Strengths and limitations

Liquid resin is cured by light, layer by layer. It gives the finest detail and the smoothest surface of all the printing processes.

Strengths

  • Smooth surface straight off the printer
  • Knurling, lettering and fine grooves come out clean

Limitations

  • Standard resin is brittle under impact
  • Does not like long exposure to sunlight
  • Needs supports and post-curing

Materials: Standard, tough and flexible resins.

When printing isn't enough, we design for metal.

High loads, high temperature or thousands of parts. We do the documentation; vetted Polish workshops do the making.

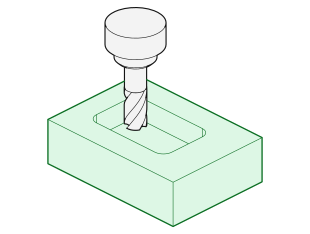
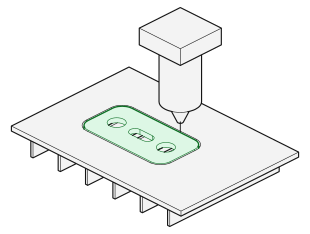
Drawing: cnc milling
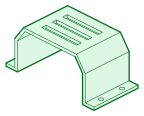
CNC millingThe shape cut from a solid block of metal.
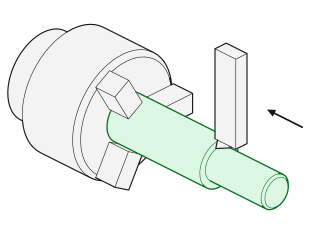
Drawing: turning
TurningShafts, bushings and external threads.
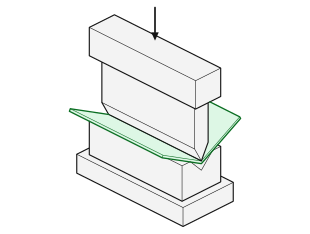
Drawing: sheet bending
Sheet bendingEnclosures, brackets and guards from one sheet.
Drawing: laser cutting
Laser cuttingThe outline straight from a DXF file, no tooling.
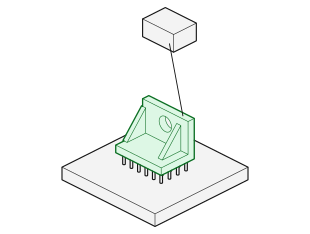
Drawing: metal printing
Metal printingA laser melts metal powder layer by layer.
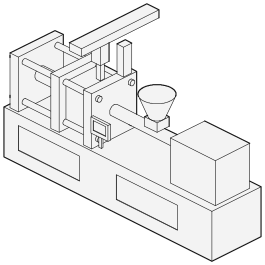
Drawing: injection mould
Injection mouldThousands of parts, the lowest unit price.

What we don't print

Frames and load-bearing members, blades, sliding pairs and parts next to an engine or a furnace. Those we make in metal, and for thousands of parts a mould pays off.

One contact

We do the documentation. Vetted workshops we work with mill, turn, cut and bend. You talk to one person.

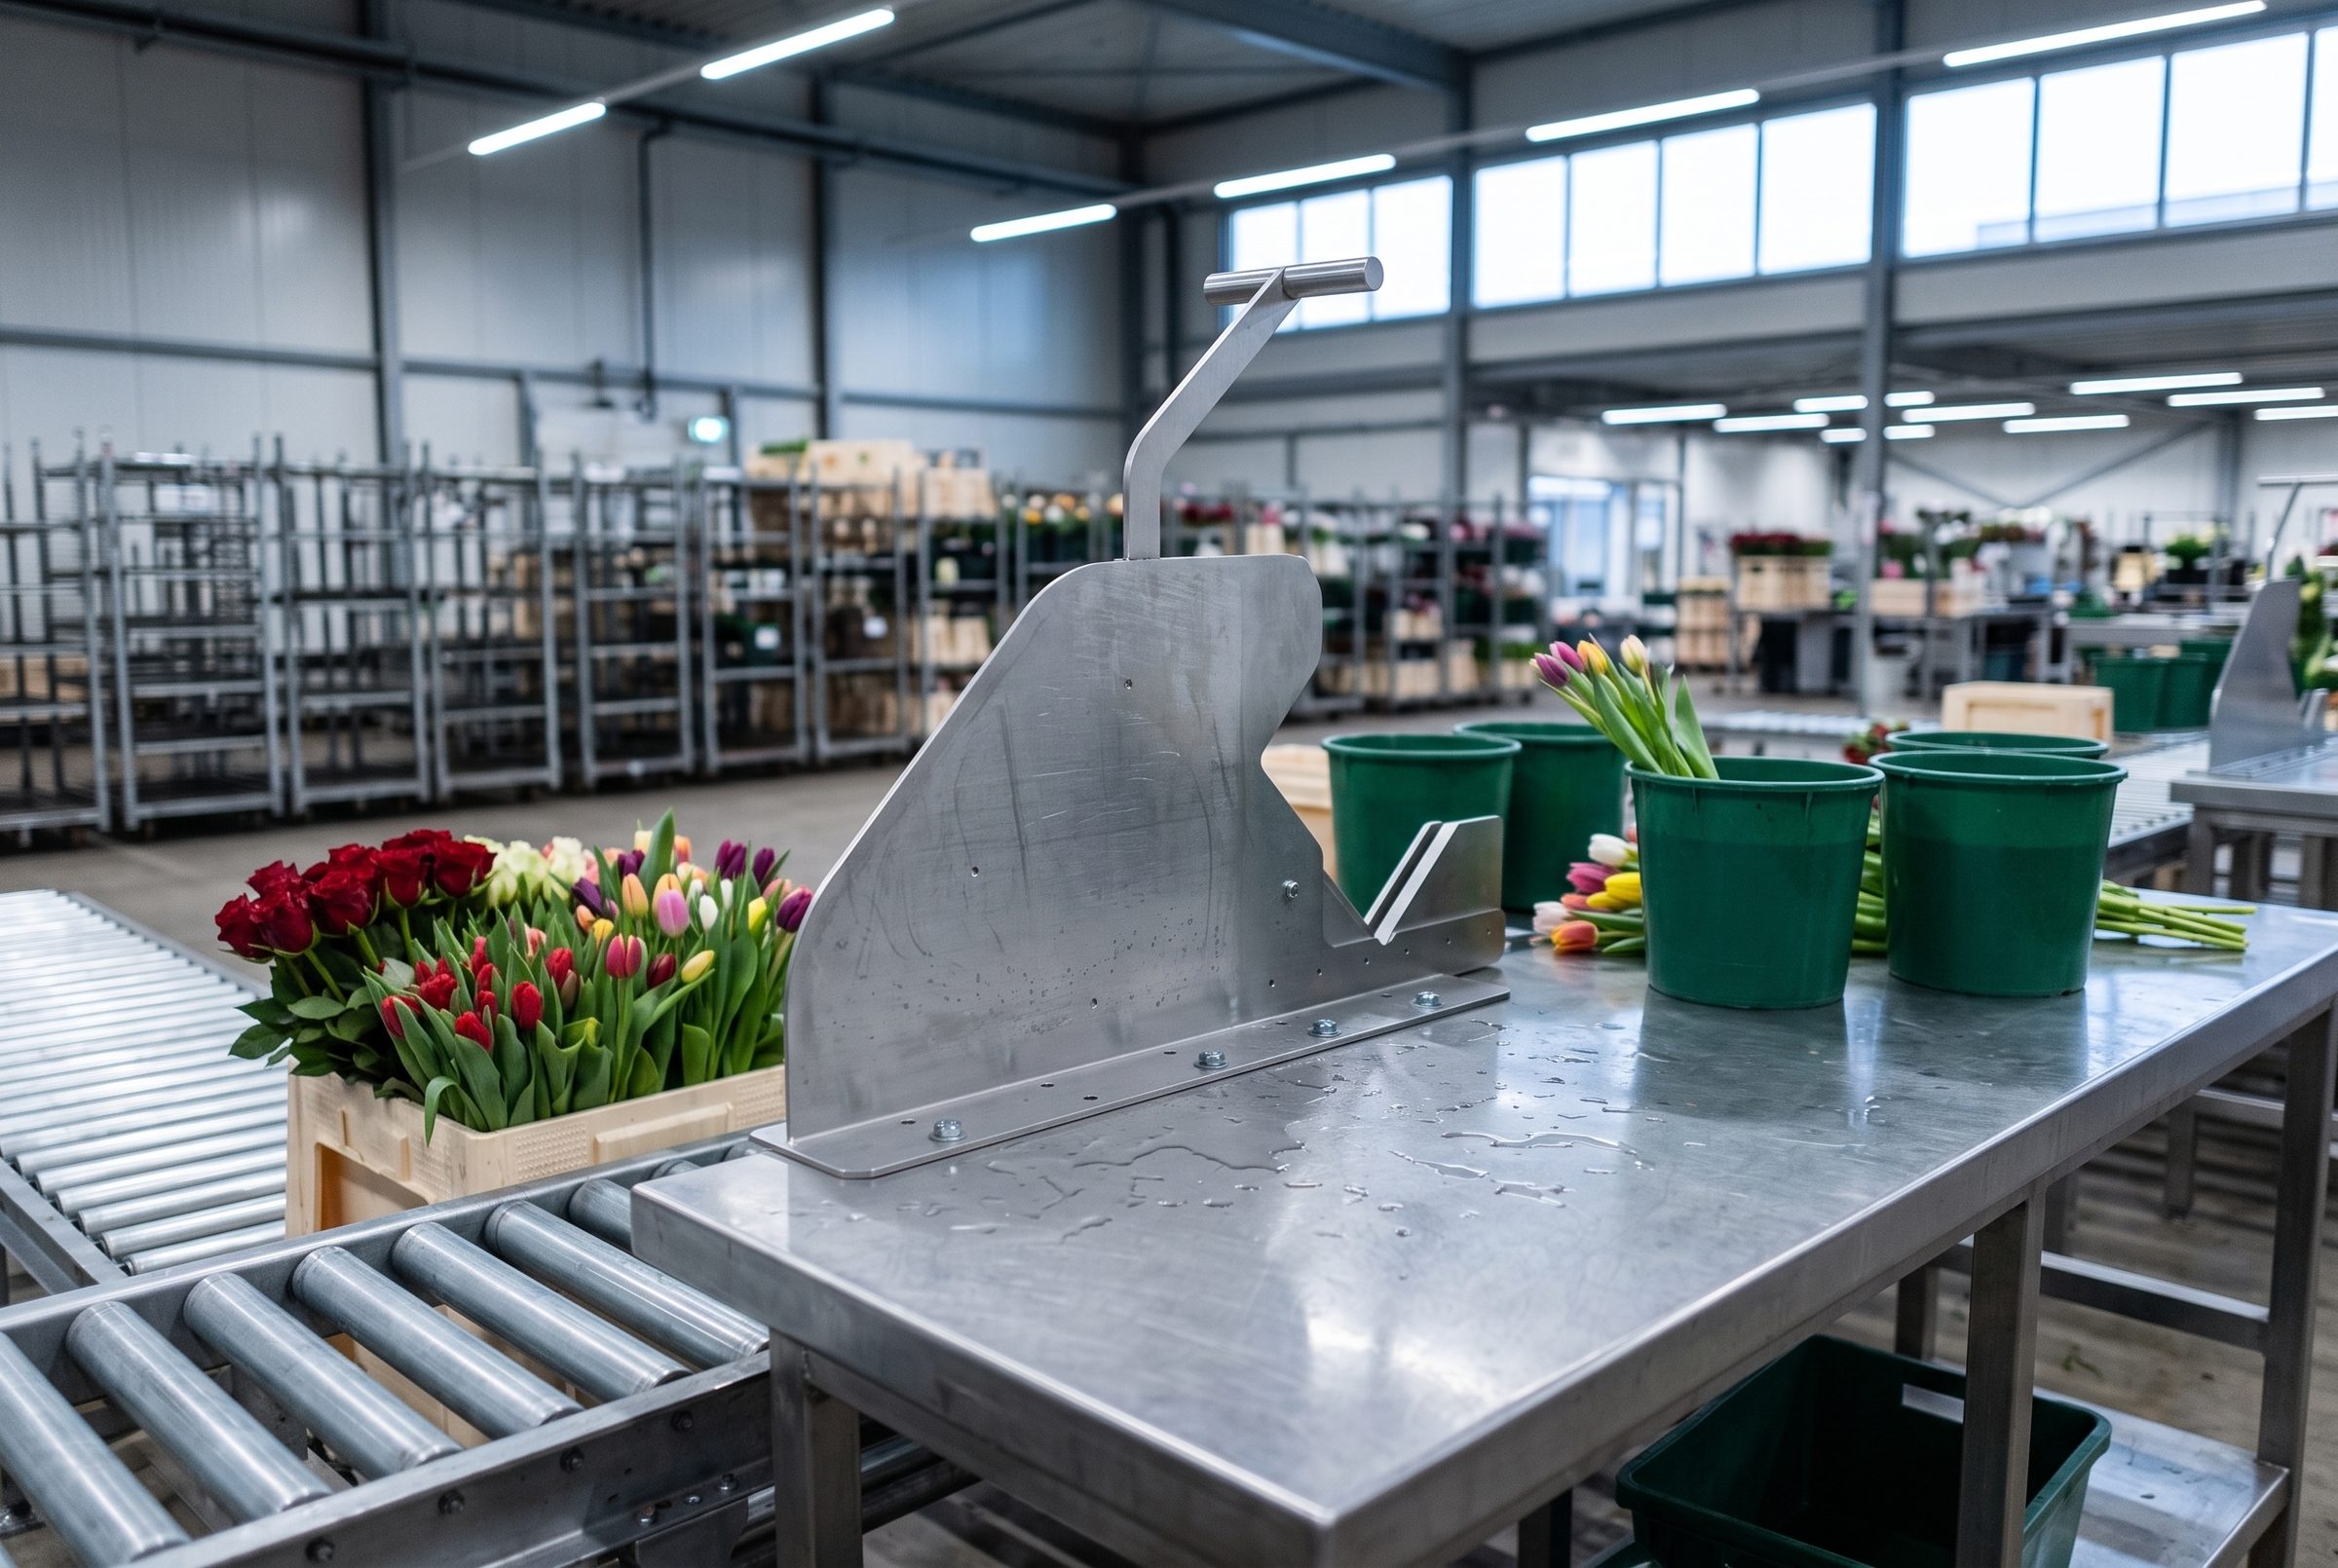
Visualisation: flower cutter in a packing hall

Not every part should be printed.

We rebuilt a flower-stem guillotine from a machine with no documentation. 4-5 mm steel and bent sheet, so printing made no sense: the client got 13 STEP files, 6 DXF profiles and 6 A3 drawings.

A material chosen for where the part will work.

The materials we use most and what they cope with. In green, the ones we reach for most often.

MaterialWhere it worksstrengthheatweatheroil
PLAFDMmock-ups and models
PETGFDMholders, guards, workshop
ASAFDMoutdoors, sun and frost
TPUFDM · powderflexible, seals, bumpers
PA12MJF · SLSmachine parts, runs
PA11MJF · SLShinges and snaps that flex
ResinSLA · DLPdetail, patterns, models
AluminiumCNCplates, bodies, light frames
SteelCNCshafts, axles, load-bearing parts

The dots are a rough rating against the rest of the table.

Beyond printingPOMPA6MDF and plywoodAcrylicSheet metalMoulding plastics

Not sure which material?

Tell us where the part works: temperature, load, contact with oil, sun and UV. We will pick the material and explain why.

Full material list
Materials
MaterialKey propertyTypical useProcess
PLAStiff, accurate, easy to print; softens in heatMock-ups, display models, stampsFDM
PETGTougher than PLA, slightly springy, moisture resistantHolders, covers, functional partsFDM
ABS / ASAHandle higher temperatures; ASA also resists UVHousings, car parts, outdoor partsFDM
TPUFlexible, rubber-likeBumpers, covers, sealsFDM
PA12All-round polyamide, strong and stableHousings, holders, adapters, functional partsMJF, SLS
PA11More impact resistant and flexible than PA12Living hinges, snap fits, parts that flexMJF, SLS
Powder TPUElastomer without supports, lattices possibleCushioning, seals, coversMJF, SLS
Standard resinVery smooth, fine detail, brittlePresentation models, figurines, mastersSLA / DLP
Tough / flexible resinResin detail with better toughness or flexibilitySmall functional parts, snaps, flexible coversSLA / DLP
AluminiumLight, stiff, machines wellEnclosures, mounting plates, machine partsCNC
SteelHighest strength and hardnessShafts, pins, load-bearing partsCNC
POMLow friction, stiff, dimensionally stableGears, guides, plain bushingsCNC
PA6Engineering polyamide, wear resistantRollers, bushings, sliding partsCNC
MDF, plywoodLarge format, light, easy to machine and paintDecorative panels and walls, templates, models, fit-outsPanel milling
Acrylic (PMMA)Clear or tinted, rigid, glossyGuards, signs, display cases, light elementsPanel milling, laser
Steel, stainless and aluminium sheetStiff and cheap in series, laser cut and bentEnclosures, brackets, frames, machine guardsLaser and bending
PP, ABS, PA, PCInjection grades: lowest unit price in large runsHousings, clips, mass-produced partsInjection moulding

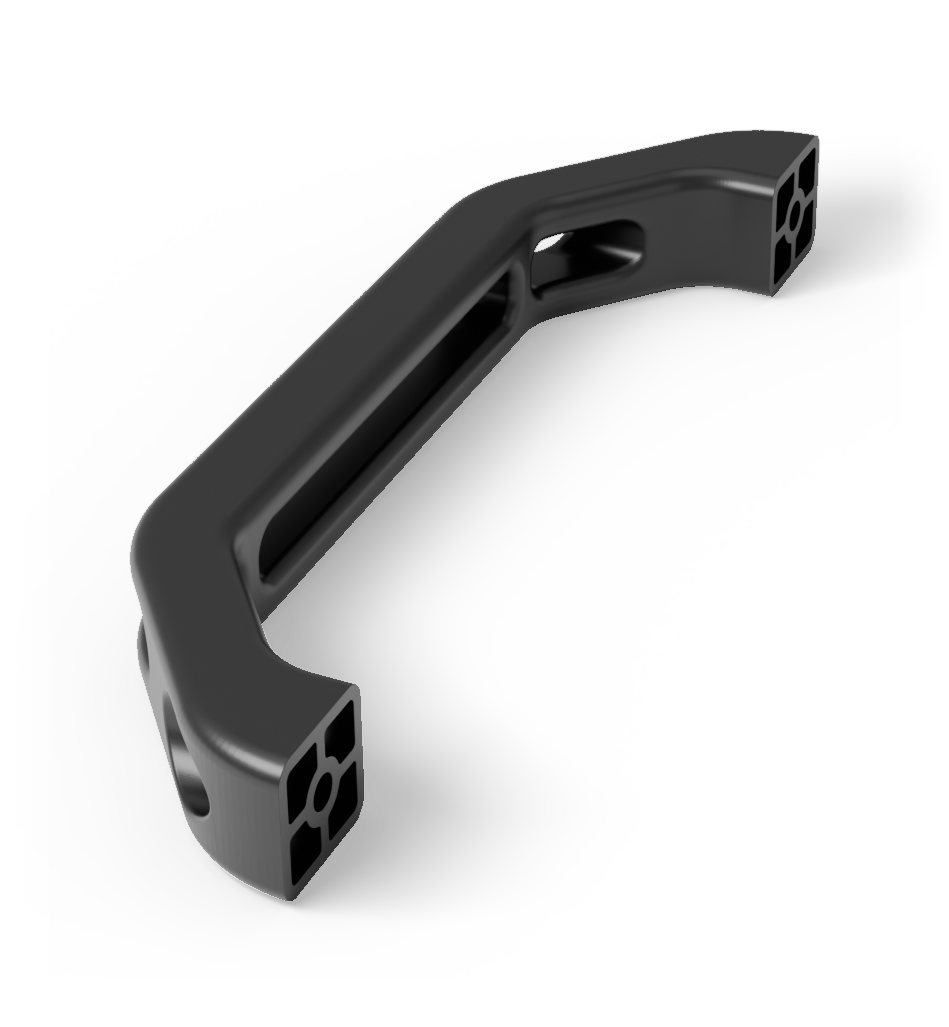
A finish changes the look and feel, not the shape.

The same part, a different finish. Each usually adds 1-3 days.

MJF

Grey off the machine. We dye it black or dark colours and vapour-smooth it to a satin surface.

  • Raw, grey
    Raw, grey
  • Dyed black
    Dyed black
  • Dyed a dark colour
    Dyed a dark colour
  • Vapour-smoothed
    Vapour-smoothed

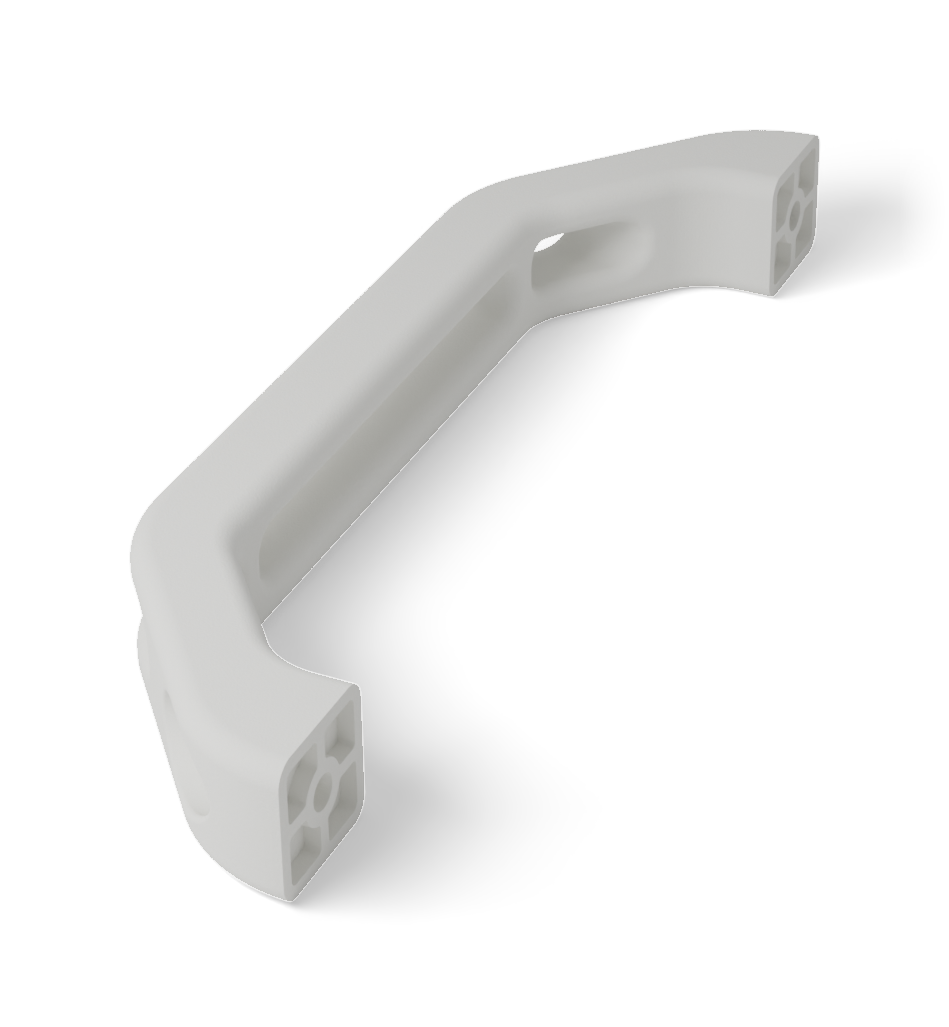
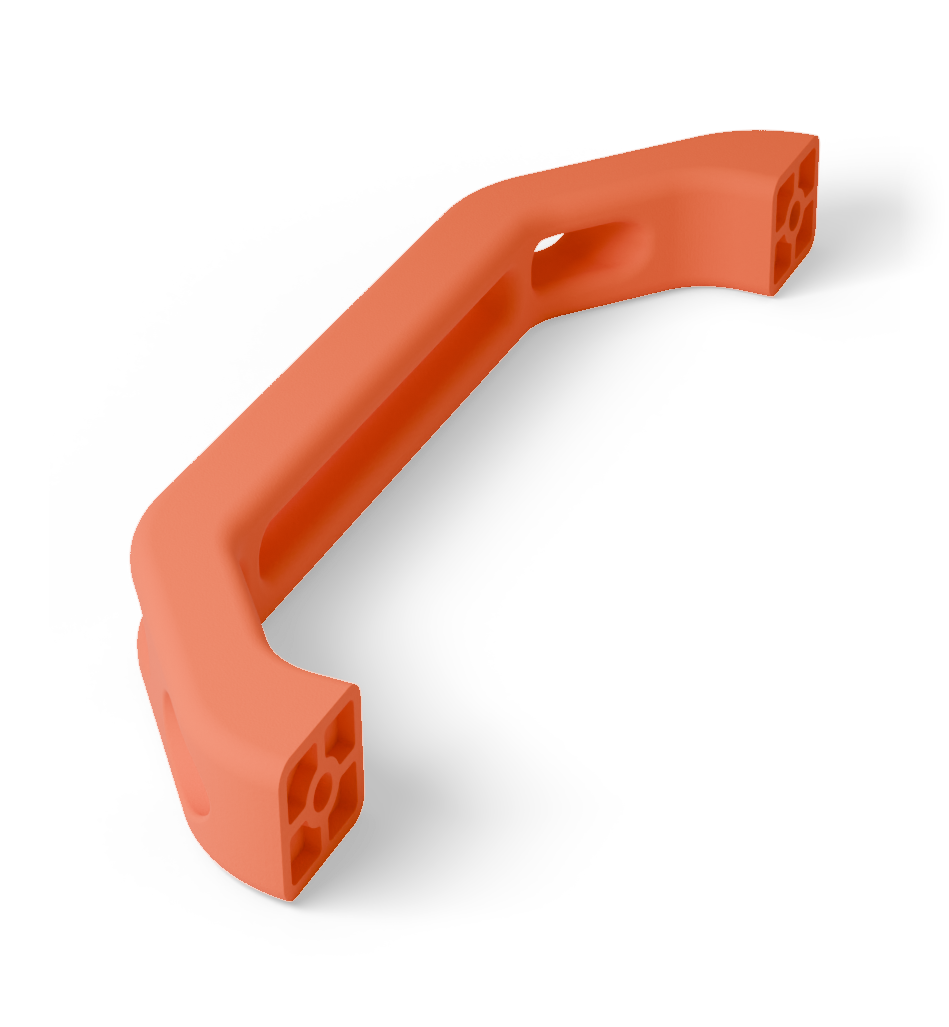
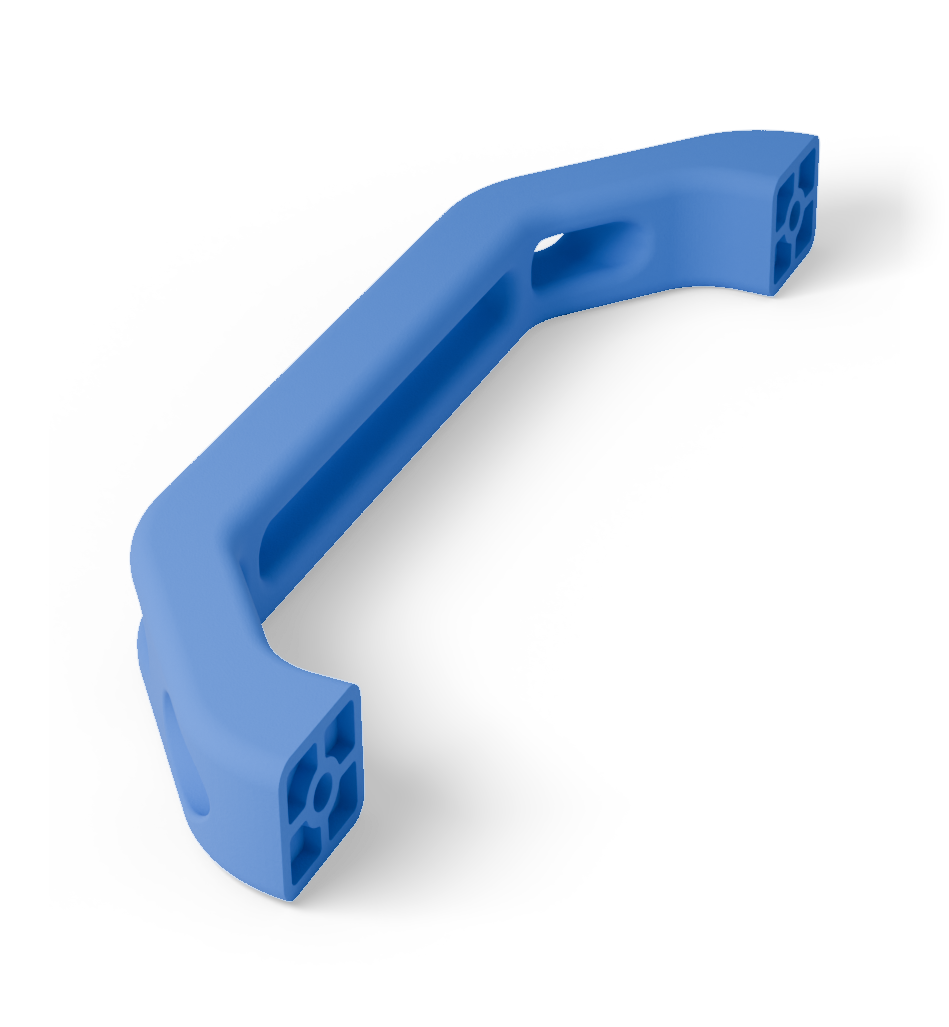
SLS and paint

SLS is white, so it also takes light colours. Paint covers anything, your brand colour included.

  • Raw SLS, white
    Raw SLS, white
  • SLS dyed orange
    SLS dyed orange
  • SLS dyed blue
    SLS dyed blue
  • Opaque paint
    Opaque paint
The five finishes in brief

Raw. Depowdered and left as is. Powder colour: grey from MJF, white from SLS. Fastest and cheapest.

Dyeing. Colour soaks into the outer layer, so it does not peel. Black or colours; light colours only from SLS.

Vapour smoothing. Solvent vapour smooths and seals the surface. The part feels smooth, cleans more easily and looks closer to a moulded part.

Painting. An even, opaque colour, including brand colours like the green and orange in the photo.

Bead blasting. A stream of fine media cleans and evens out the surface, leaving a uniform matte look.

Send a file or a photo. We reply with a price and a lead time.

STL, STEP, a drawing, a photo with dimensions or a one-line description. If something is missing, we will ask.